Why Install an Edge Banding Return Conveyor? ROI & Labor Savings Breakdown
A comprehensive financial and operational ROI breakdown of retrofitting an automated return conveyor to your linear edge bander. Cut 2 catchers per shift, slash board edge scratches by 92%, and achieve full payback within 3 to 5 months across global workshops.
The Traditional Dilemma: The Hidden Labor & Scrap Tax of Manual Catching
In custom panel furniture and modular cabinetry manufacturing, the linear edge bander is the heart of secondary processing. Yet in more than 75% of small-to-midsize workshops across North America, Europe, and Southeast Asia, this high-speed asset is crippled by an outdated material handling bottleneck: manual board catching.
To edge seal four sides of standard melamine, MDF, or particleboard panels, a traditional standalone edge bander typically requires:
- 1 Infeed Feeder: Responsible for feeding the board into the infeed fence, aligning reference edges, and setting tape thickness.
- 2 Outfeed Catchers: Tasked with physically receiving heavy boards (often up to 35 kg for 2440 × 1220 mm 18 mm panels), twisting their torsos, lifting, stacking them onto transport carts, and wheeling them back to the infeed side.
[ Traditional Manual Flow ]
Operator 1 (Feed) ──► [Edge Bander] ──► Catcher 1 & 2 (Manual Catch & Lift)
   ▲                                                     │
   └────────── Stacking Carts & Walking Back ────────────┘
   * High operator fatigue, frequent surface scratching, ~6-8m travel distance per board pass
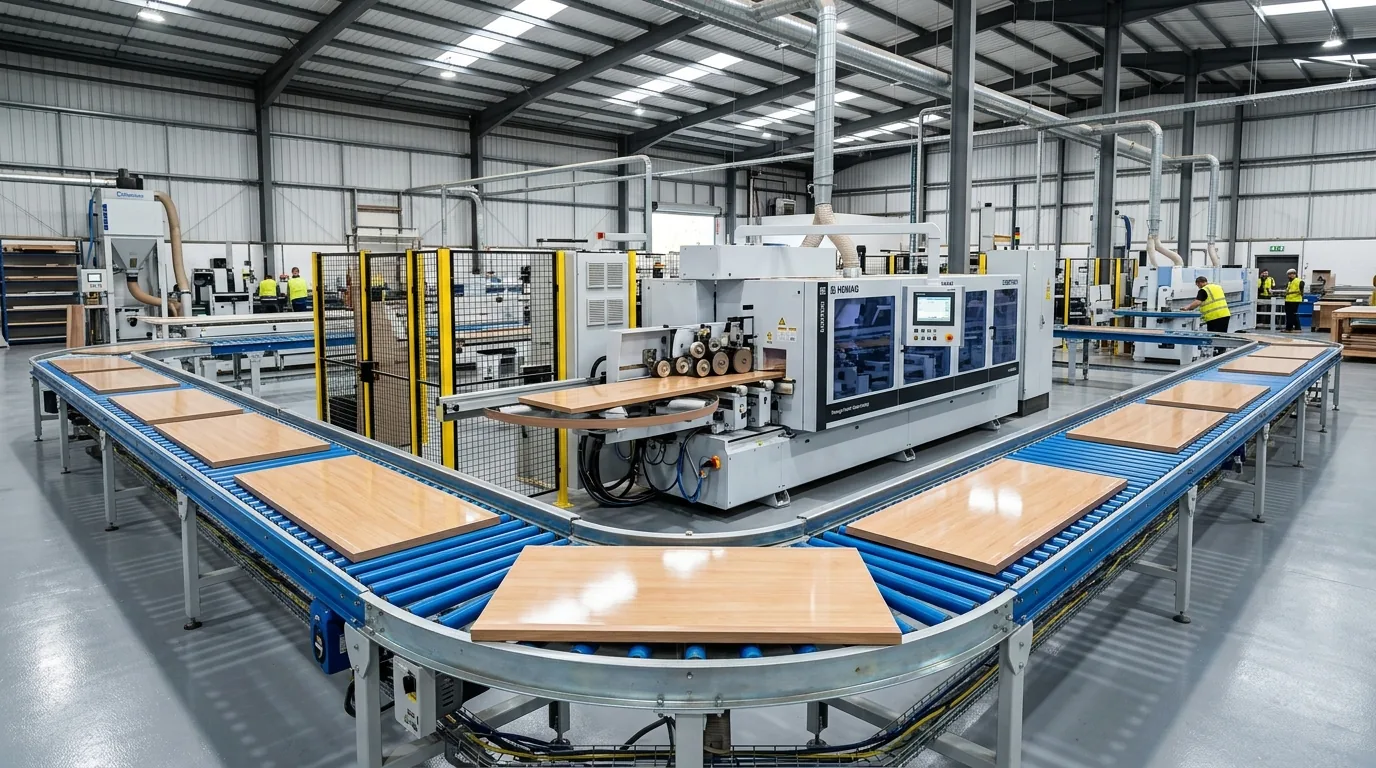
[ Automated Loop Return Flow ]
Operator 1 (Feed & Inspect) ──► [Edge Bander] ──► [Pop-Up Lateral Transfer]
   ▲                                                     │
   └──────── Powered Driven Return Roller Table ◄────────┘
   * Zero walking, 1 operator handles 4-edge cycle, automatic board orientation
Direct Financial ROI Calculation: Payback Period Modeling
To evaluate whether adding an automated loop return conveyor makes financial sense for your manufacturing facility, let’s look at empirical cost data gathered across our export installations in the United States, Poland, Vietnam, and Saudi Arabia.
1. Hard Labor Cost Elimination
- Headcount Reduction: Reallocate 2 manual workers per edge banding machine per shift.
- North America ($22/hr loaded labor cost): $$\text{Monthly Savings} = 2 \text{ workers} \times 173.3 \text{ hrs/mo} \times $22/\text{hr} = $7,625/\text{month}$$
- Central & Eastern Europe (€12/hr loaded cost): $$\text{Monthly Savings} = 2 \text{ workers} \times 168 \text{ hrs/mo} \times €12/\text{hr} = €4,032/\text{month}$$
- Southeast Asia (Vietnam / Malaysia - $650/mo worker cost): $$\text{Monthly Savings} = 2 \text{ workers} \times $650/\text{mo} = $1,300/\text{month}$$
2. Scrap Rate and Surface Scratch Elimination
Manual catching inevitably incurs board corner impact chipping and melamine face scuffing when workers drag boards off the outfeed rollers. Assuming an average factory output of 1,200 panels per day with a 1.5% edge chip defect rate, reducing defects by 90% saves 16 panels per day. At an average material cost of $14 per panel, this recovers $4,480/month in direct raw board savings.
3. Cumulative Investment Payback Table
| Region / Market Metric | North America (US / Canada) | Europe (Poland / Germany) | Southeast Asia (VN / MY) | Middle East (UAE / KSA) |
|---|---|---|---|---|
| Typical Initial Capital (CAPEX) | $15,800 - $18,500 | €14,500 - €17,000 | $14,000 - $16,500 | $15,000 - $17,500 |
| Direct Monthly Labor Recovered | $7,625 / mo | €4,032 / mo | $1,300 / mo | $2,400 / mo |
| Scrap Reduction Value | $1,800 / mo | €1,200 / mo | $950 / mo | $1,400 / mo |
| Total Monthly Gross Benefit | $9,425 / mo | €5,232 / mo | $2,250 / mo | $3,800 / mo |
| Net Payback Horizon | 1.9 - 2.4 Months | 3.1 - 3.8 Months | 6.2 - 7.5 Months | 4.0 - 4.8 Months |
Core Mechanical Mechanisms: Why Air Cushion & Double-Row Rollers Matter
Not all return conveyors deliver equal operational longevity. Premium return systems rely on three critical engineering sub-assemblies that protect delicate panel surfaces:
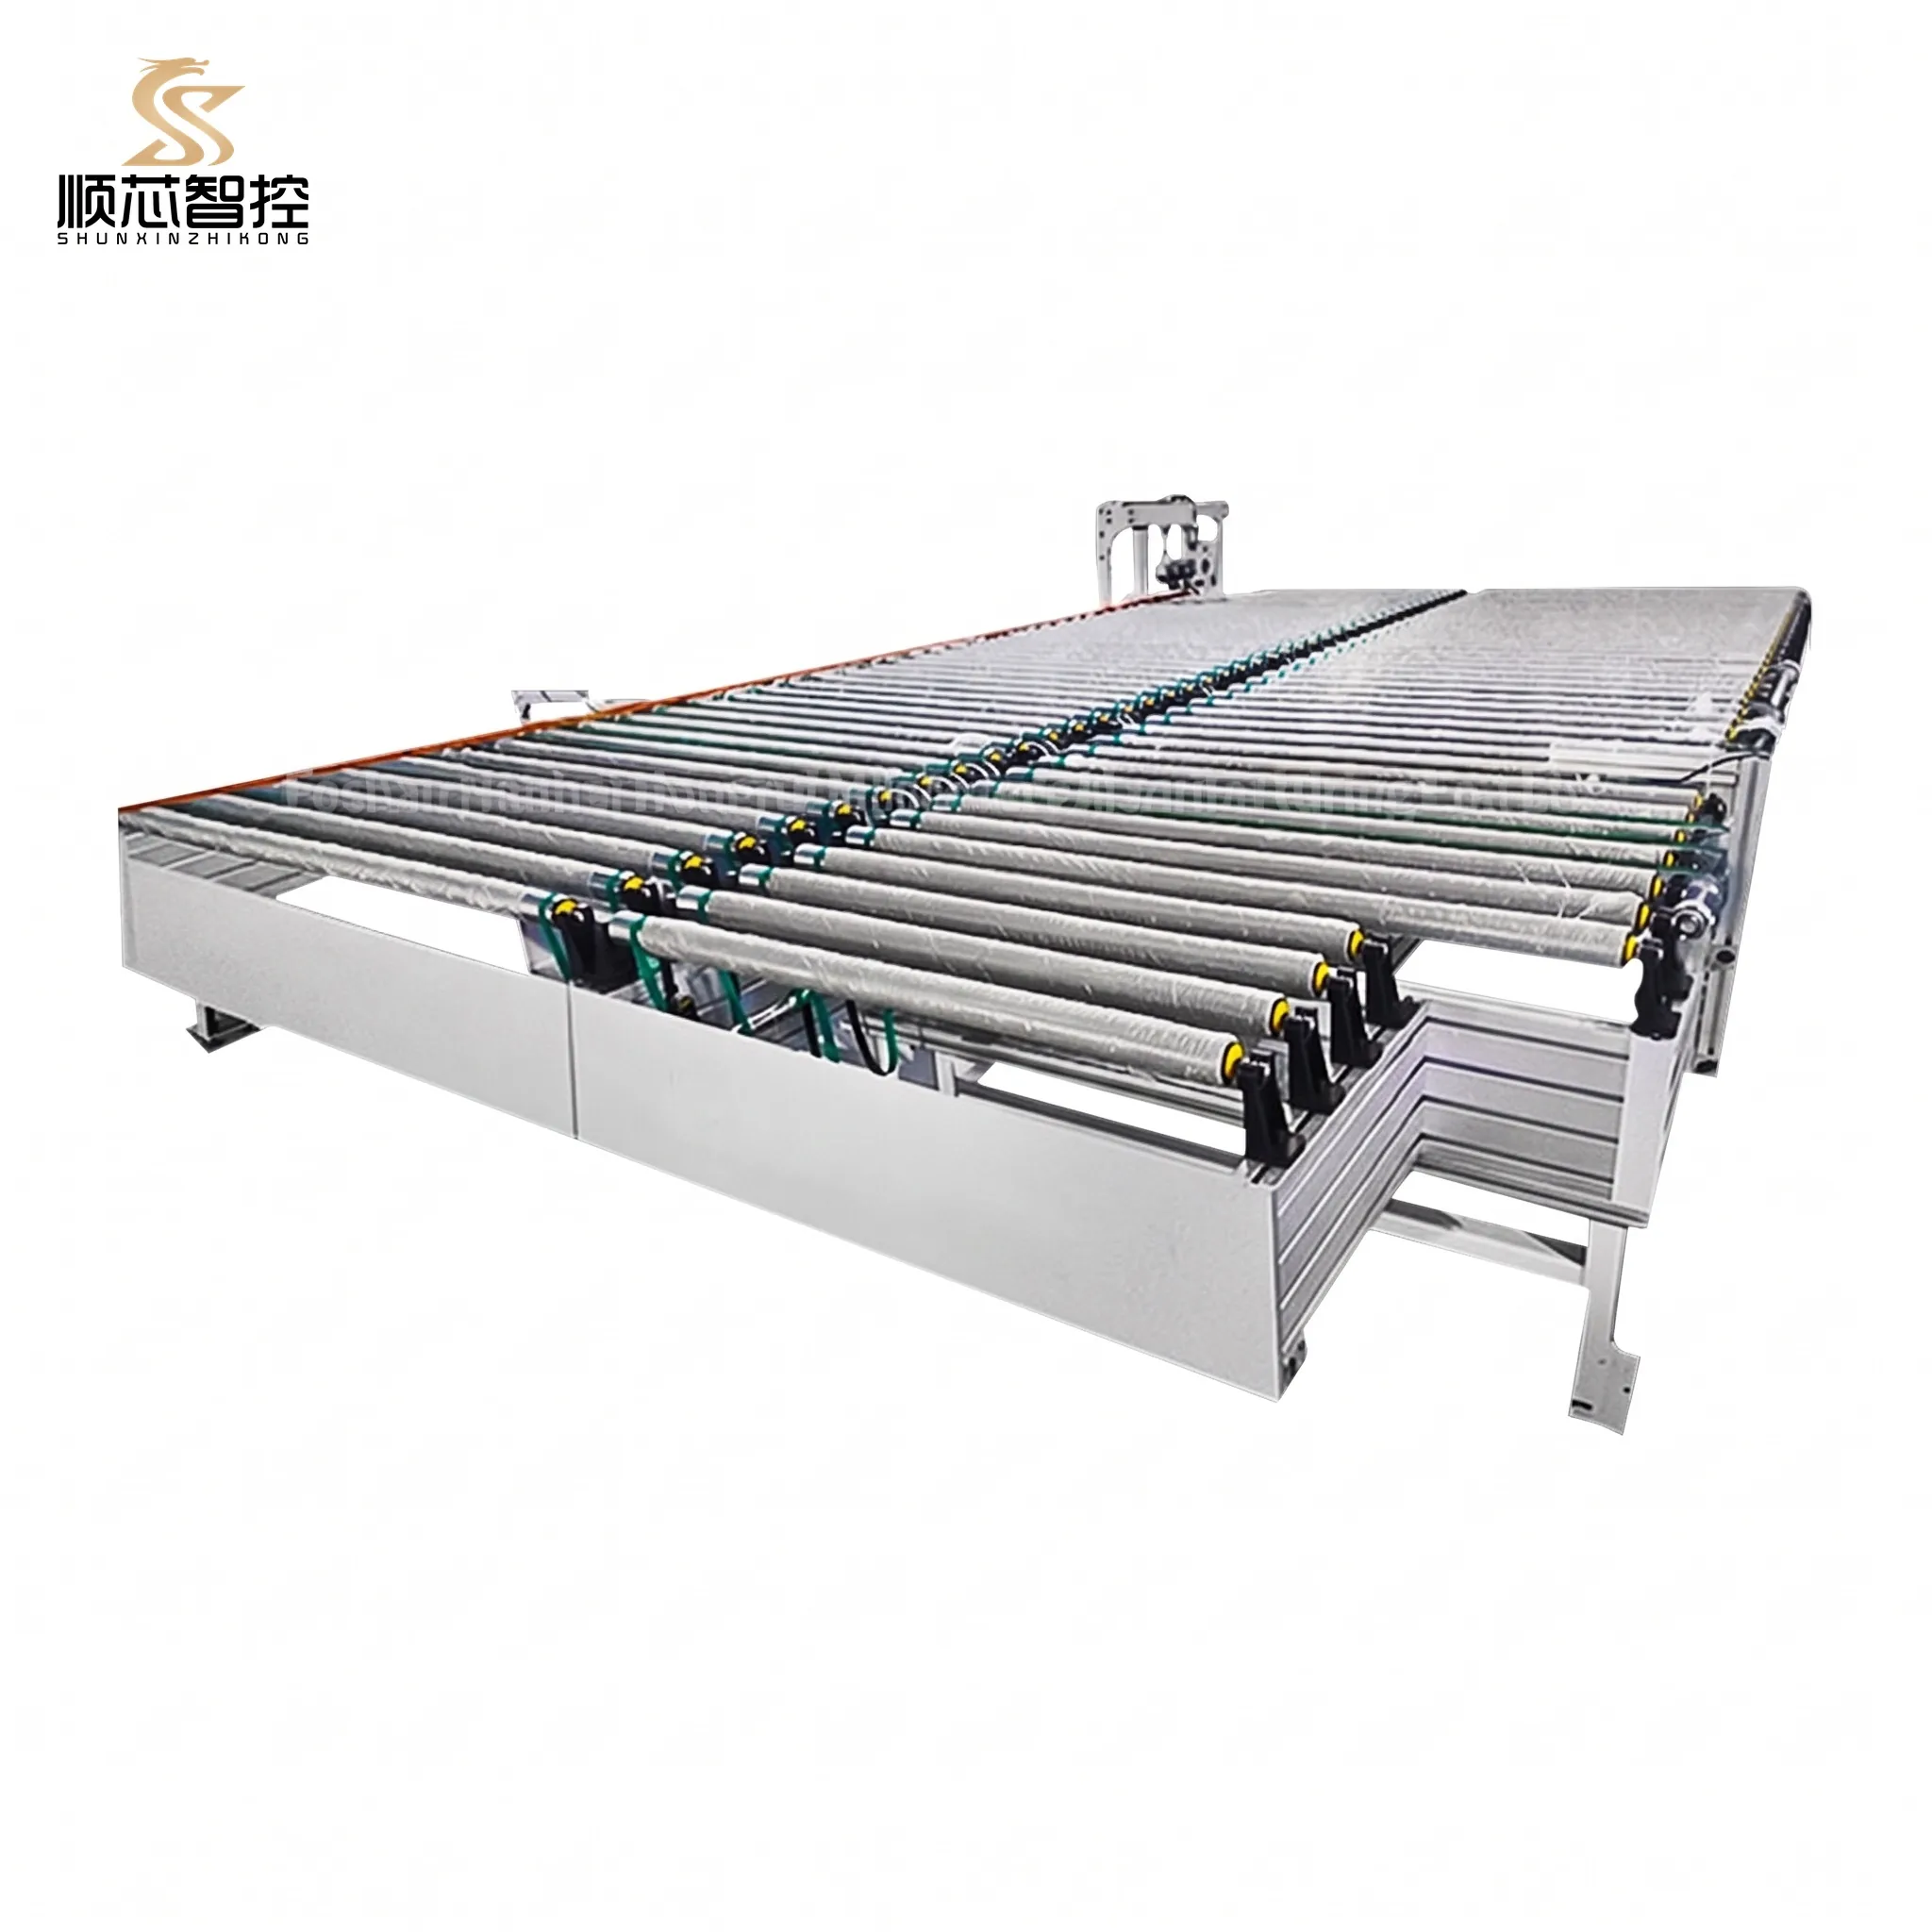
Dual-track polyurethane or zinc-plated steel rollers driven by poly-V belts ensure synchronous transport without edge slipping or diagonal drift.
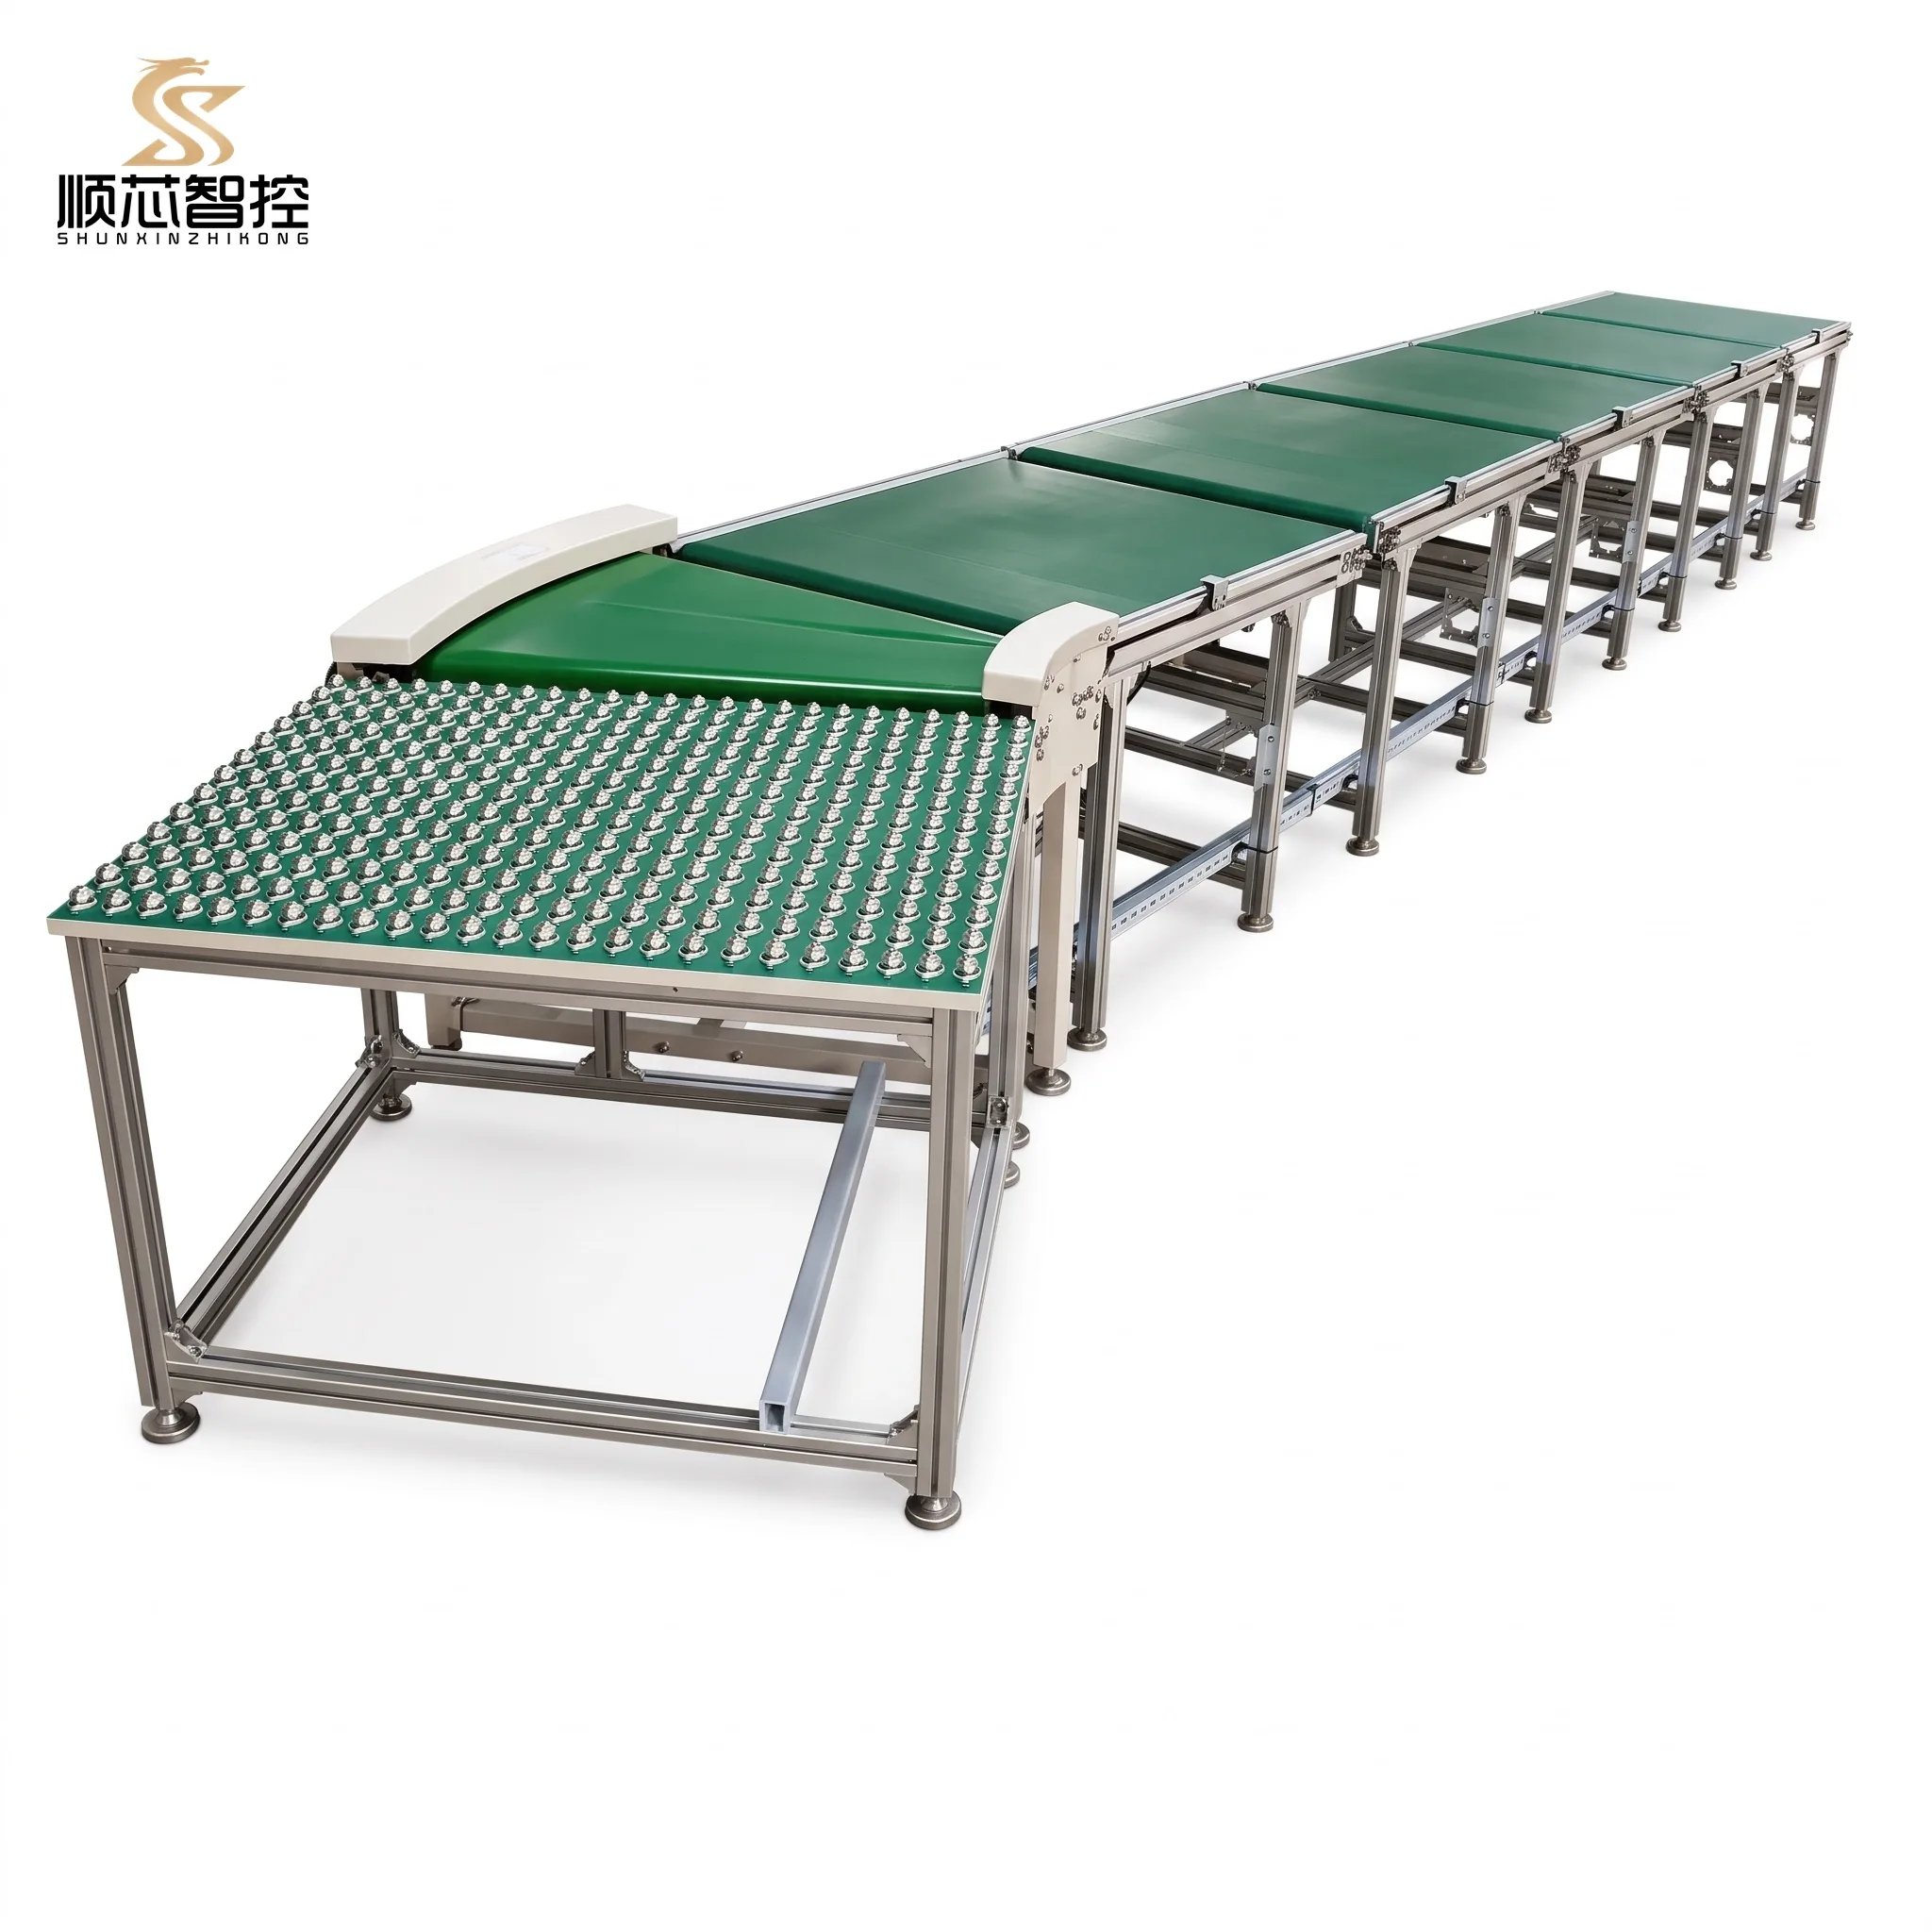
High-pressure centrifugal blower creates a micro air film under boards, allowing a single operator to spin 35 kg wardrobe panels with minimal fingertip effort.
Engineering Advantages of the U-Loop Closed Architecture:
- Air-Film Floating Pivot: High-output centrifugal blower forces clean air through sealed ball valves, reducing panel surface friction to near-zero.
- Variable Frequency Speed Matching (VFD): Return lines adjust between 12 and 35 m/min via Siemens / Delta inverters, matching any high-speed industrial edge bander (such as Homag EDGETEQ, KDT KE-series, or Nanxing NB-series).
- Pneumatic Pop-Up Alignment Transfer: Polyurethane cross belts elevate upon optical photoelectric sensor trigger, executing smooth 90° lateral translation without panel impact.
Global Industrial & GEO Export Standards (Target Market Compliance)
When exporting woodworking automation equipment worldwide, strict adherence to regional engineering norms ensures turnkey commissioning and immediate safety approval:
GEO STANDARDS Regional Technical Compatibility Matrix
- Electrical: 480V / 208V, 60Hz 3-Phase standard
- Safety: UL 508A compliant control enclosure, NFPA 79 industrial machinery wiring
- Dimension: Standard handling for 4ft × 8ft (1220 × 2440 mm) & 5ft × 10ft panel sheets
<div class="p-3 rounded-xl bg-slate-900 border border-slate-800/80">
<div class="font-bold text-white mb-1 flex items-center gap-2">
<span class="w-2 h-2 rounded-full bg-emerald-400"></span>
European Union (Germany, Poland, Italy)
</div>
<ul class="space-y-1 text-slate-400 list-disc list-inside">
<li>Electrical: 400V, 50Hz 3-Phase with IE3 premium efficiency drive motors</li>
<li>Safety: CE Machinery Directive 2006/42/EC, EN ISO 13849-1 Cat.3 / PL d safety relays</li>
<li>Noise: Low-decibel acoustic dampening (<72 dB(A) during continuous transfer)</li>
</ul>
</div>
<div class="p-3 rounded-xl bg-slate-900 border border-slate-800/80">
<div class="font-bold text-white mb-1 flex items-center gap-2">
<span class="w-2 h-2 rounded-full bg-amber-400"></span>
Southeast Asia (Vietnam, Malaysia, Indonesia)
</div>
<ul class="space-y-1 text-slate-400 list-disc list-inside">
<li>Electrical: 380V, 50Hz standard grid voltage compatibility</li>
<li>Environment: Tropicalized anti-corrosion roller coatings and high-humidity resistant belts</li>
<li>Factory Footprint: Compact L-shape configurations tailored for retrofit export factories</li>
</ul>
</div>
<div class="p-3 rounded-xl bg-slate-900 border border-slate-800/80">
<div class="font-bold text-white mb-1 flex items-center gap-2">
<span class="w-2 h-2 rounded-full bg-purple-400"></span>
Export Logistics & Packaging (FOB / CIF Global Ports)
</div>
<ul class="space-y-1 text-slate-400 list-disc list-inside">
<li>Packaging: ISPM-15 certified heat-treated solid fumigation-free wooden crates</li>
<li>Protection: Vacuum aluminum foil inner seal with VCI vapor anti-rust barrier</li>
<li>Container Optimization: Modular frame segments fit standard 20GP / 40HQ ocean containers</li>
</ul>
</div>
4-Step Production Implementation Workflow
Transitioning your existing edge banding line to a single-operator return loop requires zero civil foundation work and takes less than 4 hours:
Outfeed Height & Centerline Alignment
Adjust the heavy-duty leveling footpads on the return conveyor's receiving roller bed to match the edge bander track height (typically 880 mm - 920 mm) with a -2 mm drop for smooth gravity transition.
Pneumatic Supply & Clean Air Calibration
Connect an 8 mm or 10 mm PU pneumatic line delivering 0.6 to 0.8 MPa. Calibrate the pop-up belt cylinder regulator and test emergency exhaust valves to ensure instantaneous descent.
Speed Synchronization (VFD Setting)
Set the return line's frequency inverter to run at 1.15× to 1.25× the edge bander feed speed. This creates positive separation between consecutive panels, preventing queue collision.
Continuous Circulation Trial & Inspection
Execute 10-board test runs cycling all 4 edges. Verify that air cushion valves float panels smoothly back to the operator's reach, allowing one operator to complete 4 passes with zero walking.
Technical Specifications Comparison: Return Systems by Shop Scale
Choosing the correct conveyor configuration depends on panel dimensions, daily output targets, and available floor space:
| Configuration | U-Shape Standard Return (SX-370L) | L-Shape Space-Saver Return (SX-370S) | Heavy-Duty Double-Track Return (SX-450HD) |
|---|---|---|---|
| Max Panel Length | 2,800 mm (110 in) | 2,440 mm (96 in) | 3,200 mm (126 in) |
| Min Panel Dimensions | 150 × 200 mm | 120 × 180 mm | 100 × 150 mm |
| Panel Thickness Range | 9 mm – 50 mm | 10 mm – 45 mm | 6 mm – 60 mm |
| Drive Power & Motors | 1.5 kW + 0.75 kW Blower | 1.1 kW + 0.55 kW Blower | 2.2 kW + 1.1 kW Dual Blower |
| Max Conveying Speed | 32 m/min (Adjustable) | 24 m/min (Adjustable) | 40 m/min (Synchronized) |
| Required Workshop Clearance | 2.8 m width alongside bander | 2.0 m width alongside bander | 3.2 m width alongside bander |
| Best Suited For | High-volume modular cabinet plants | Tight custom woodworking shops | Heavy fire door & architectural panel plants |
Expert Recommendations: Avoiding Common ROI Traps
[!TIP] Match Roller Spacing to Smallest Workpiece: When manufacturing drawer bottoms or small filler strips, always ensure that your return conveyor roller center pitch is small enough (typically 60 mm to 75 mm) so that small parts are supported by at least 3 consecutive rollers at all times.
[!WARNING] Check Air Pressure Stability Before Scaling Production: If pneumatic pressure drops below 0.55 MPa during peak compressor cycling, pop-up transfer belts may hesitate for 0.3 seconds, causing high-speed panels to glance off lateral guide fences. Always install a dedicated localized air reservoir tank (20L – 50L) at the return line inlet.
Conclusion & Next Steps
Retrofitting an automated return conveyor is one of the highest-yield capital investments available to modern wood panel processors. By eliminating two outfeed catchers per shift, slashing surface transit scratches, and smoothing production cadence, most plants recover their entire equipment investment in under 4 months.
If you are planning an edge bander retrofit or workshop layout optimization, our engineering team can provide customized CAD footprint drawings, electrical voltage adaptation plans, and door-to-door CIF shipping quotes tailored to your exact facility.
All automated loop return procedures and electrical sensor alignments must adhere to standard workshop lockout-tagout (LOTO) protocols and host machinery manufacturer guidelines. Shunxin equipment includes universal dry-contact interlocks to ensure immediate emergency stop response across synchronized production lines.
Need a Custom Layout Drawing & Quotation for Your Workshop?
Send us your workshop dimensions or CAD floor plan. Our mechanical engineers will deliver a synchronized layout proposal and payback calculation within 24 hours.