How to Eliminate Bottlenecks Between Nesting CNC Routers and Edge Banding Cells
Practical lean manufacturing engineering and automated buffer strategies to balance high-speed CNC nesting routers with linear edge banding lines. Eliminate WIP floor pile-ups, prevent barcode sorting chaos, and boost workshop throughput by 45%.
The Classic Workshop Dilemma: Batch Cutting vs. Serial Edge Sealing
In custom panel furniture and commercial architectural millwork facilities, the boundary between the Nesting CNC cutting cell and the Linear Edge Banding cell represents the single biggest bottleneck on the factory floor:
- Batch Discharges vs. Linear Intake: A high-speed nesting router cuts an entire 2440 × 1220 mm (4×8 ft) or 2800 × 1220 mm sheet in 4 to 6 minutes, discharging 18 to 35 disparate small, medium, and large parts all at once onto an outfeed belt table.
- The Sorting Scramble: The edge bander can only accept panels one piece at a time. The operator must rapidly scan barcodes, determine which edge needs sealing, and physically sift through piles of freshly routed panels.
- Severe WIP Congestion: Without automated buffers, unfinished components are stacked on manual hand carts. Pallet jacks and rolling trollies quickly choke aisle space, creating traffic hazards and leading to damaged board corners.
[ Unbuffered Bottleneck Flow ]
[CNC Nesting Router] ──(Discharges 25 parts at once)──► [Discharge Belt]
                                                             │
                    ❌ Floor Congestion (Piles on Carts) ◄────┘
                                                             │
Operator Hand-Sorts ──► [Edge Bander] (Starved or Overwhelmed)
[ Automated Lean Intralogistics Flow ]
[CNC Nesting Infeed] ──► [Nesting Cell] ──► [Automated Buffer / Sorting Conveyor]
                                                   │ (FIFO Continuous Feed)
                                                   ▼
                     [Single-Operator Edge Bander with Return Loop]
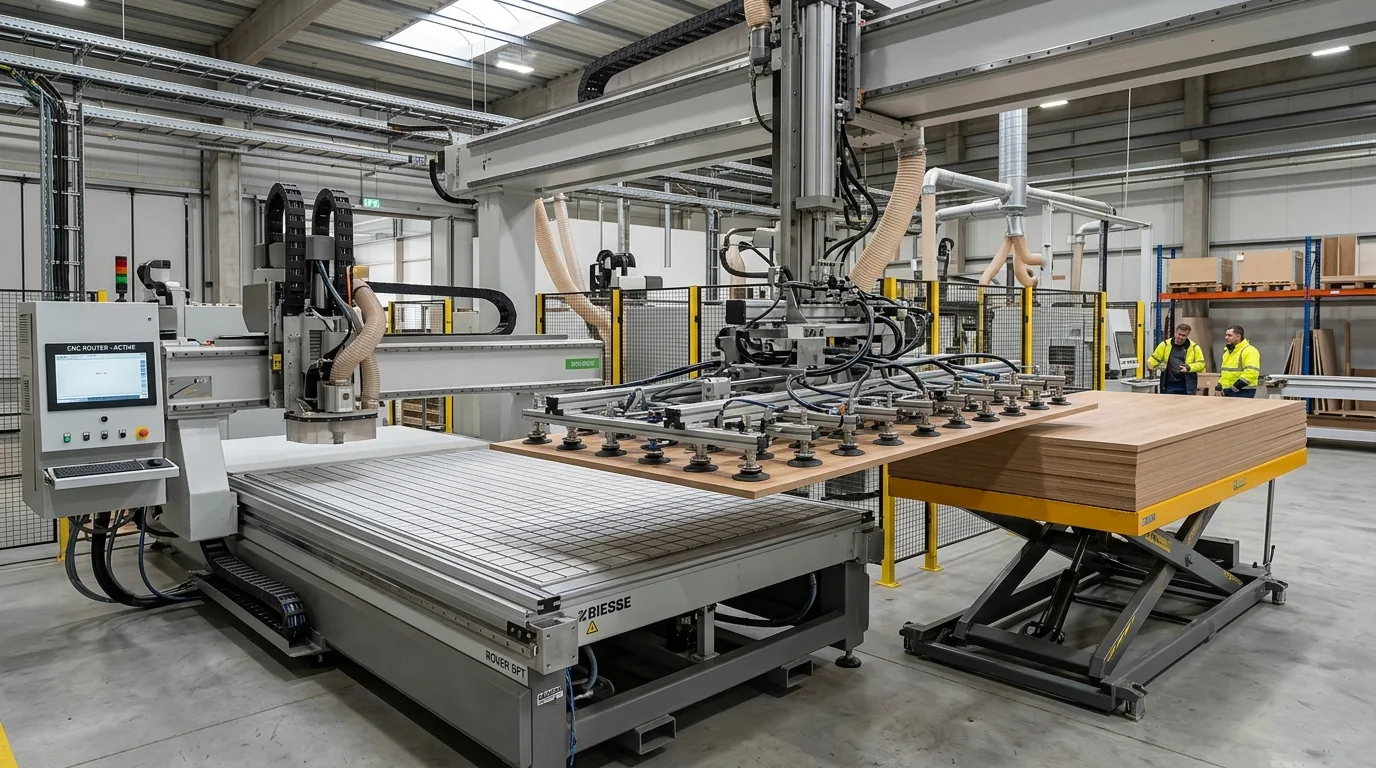
3 Core Engineering Strategies to Balance Production Cadence
To synchronize CNC nesting cutting speeds with linear edge bander intake, leading factories implement three integrated intralogistics modules:
1. Infeed Automation on Nesting Routers
Manual loading of raw MDF or melamine sheets onto the CNC table wastes up to 35% of the machine’s available cutting hours. Equipping the router with an automatic scissor lift loading table and pneumatic vacuum suction pusher allows raw sheets to load in under 20 seconds while sweeping finished parts onto the outfeed belt simultaneously.
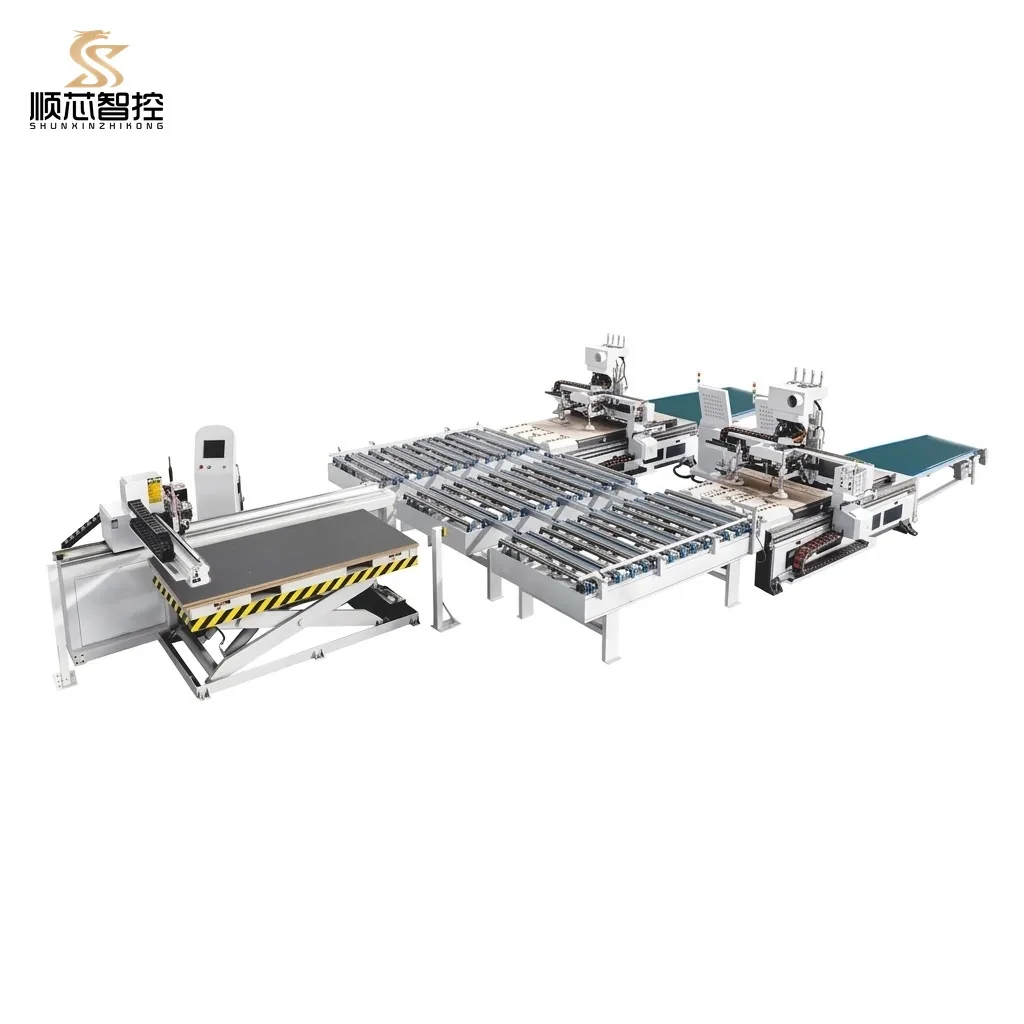
Automatic optical height tracking maintains the raw board stack at exact table height, feeding single boards instantly via motorized push rollers.
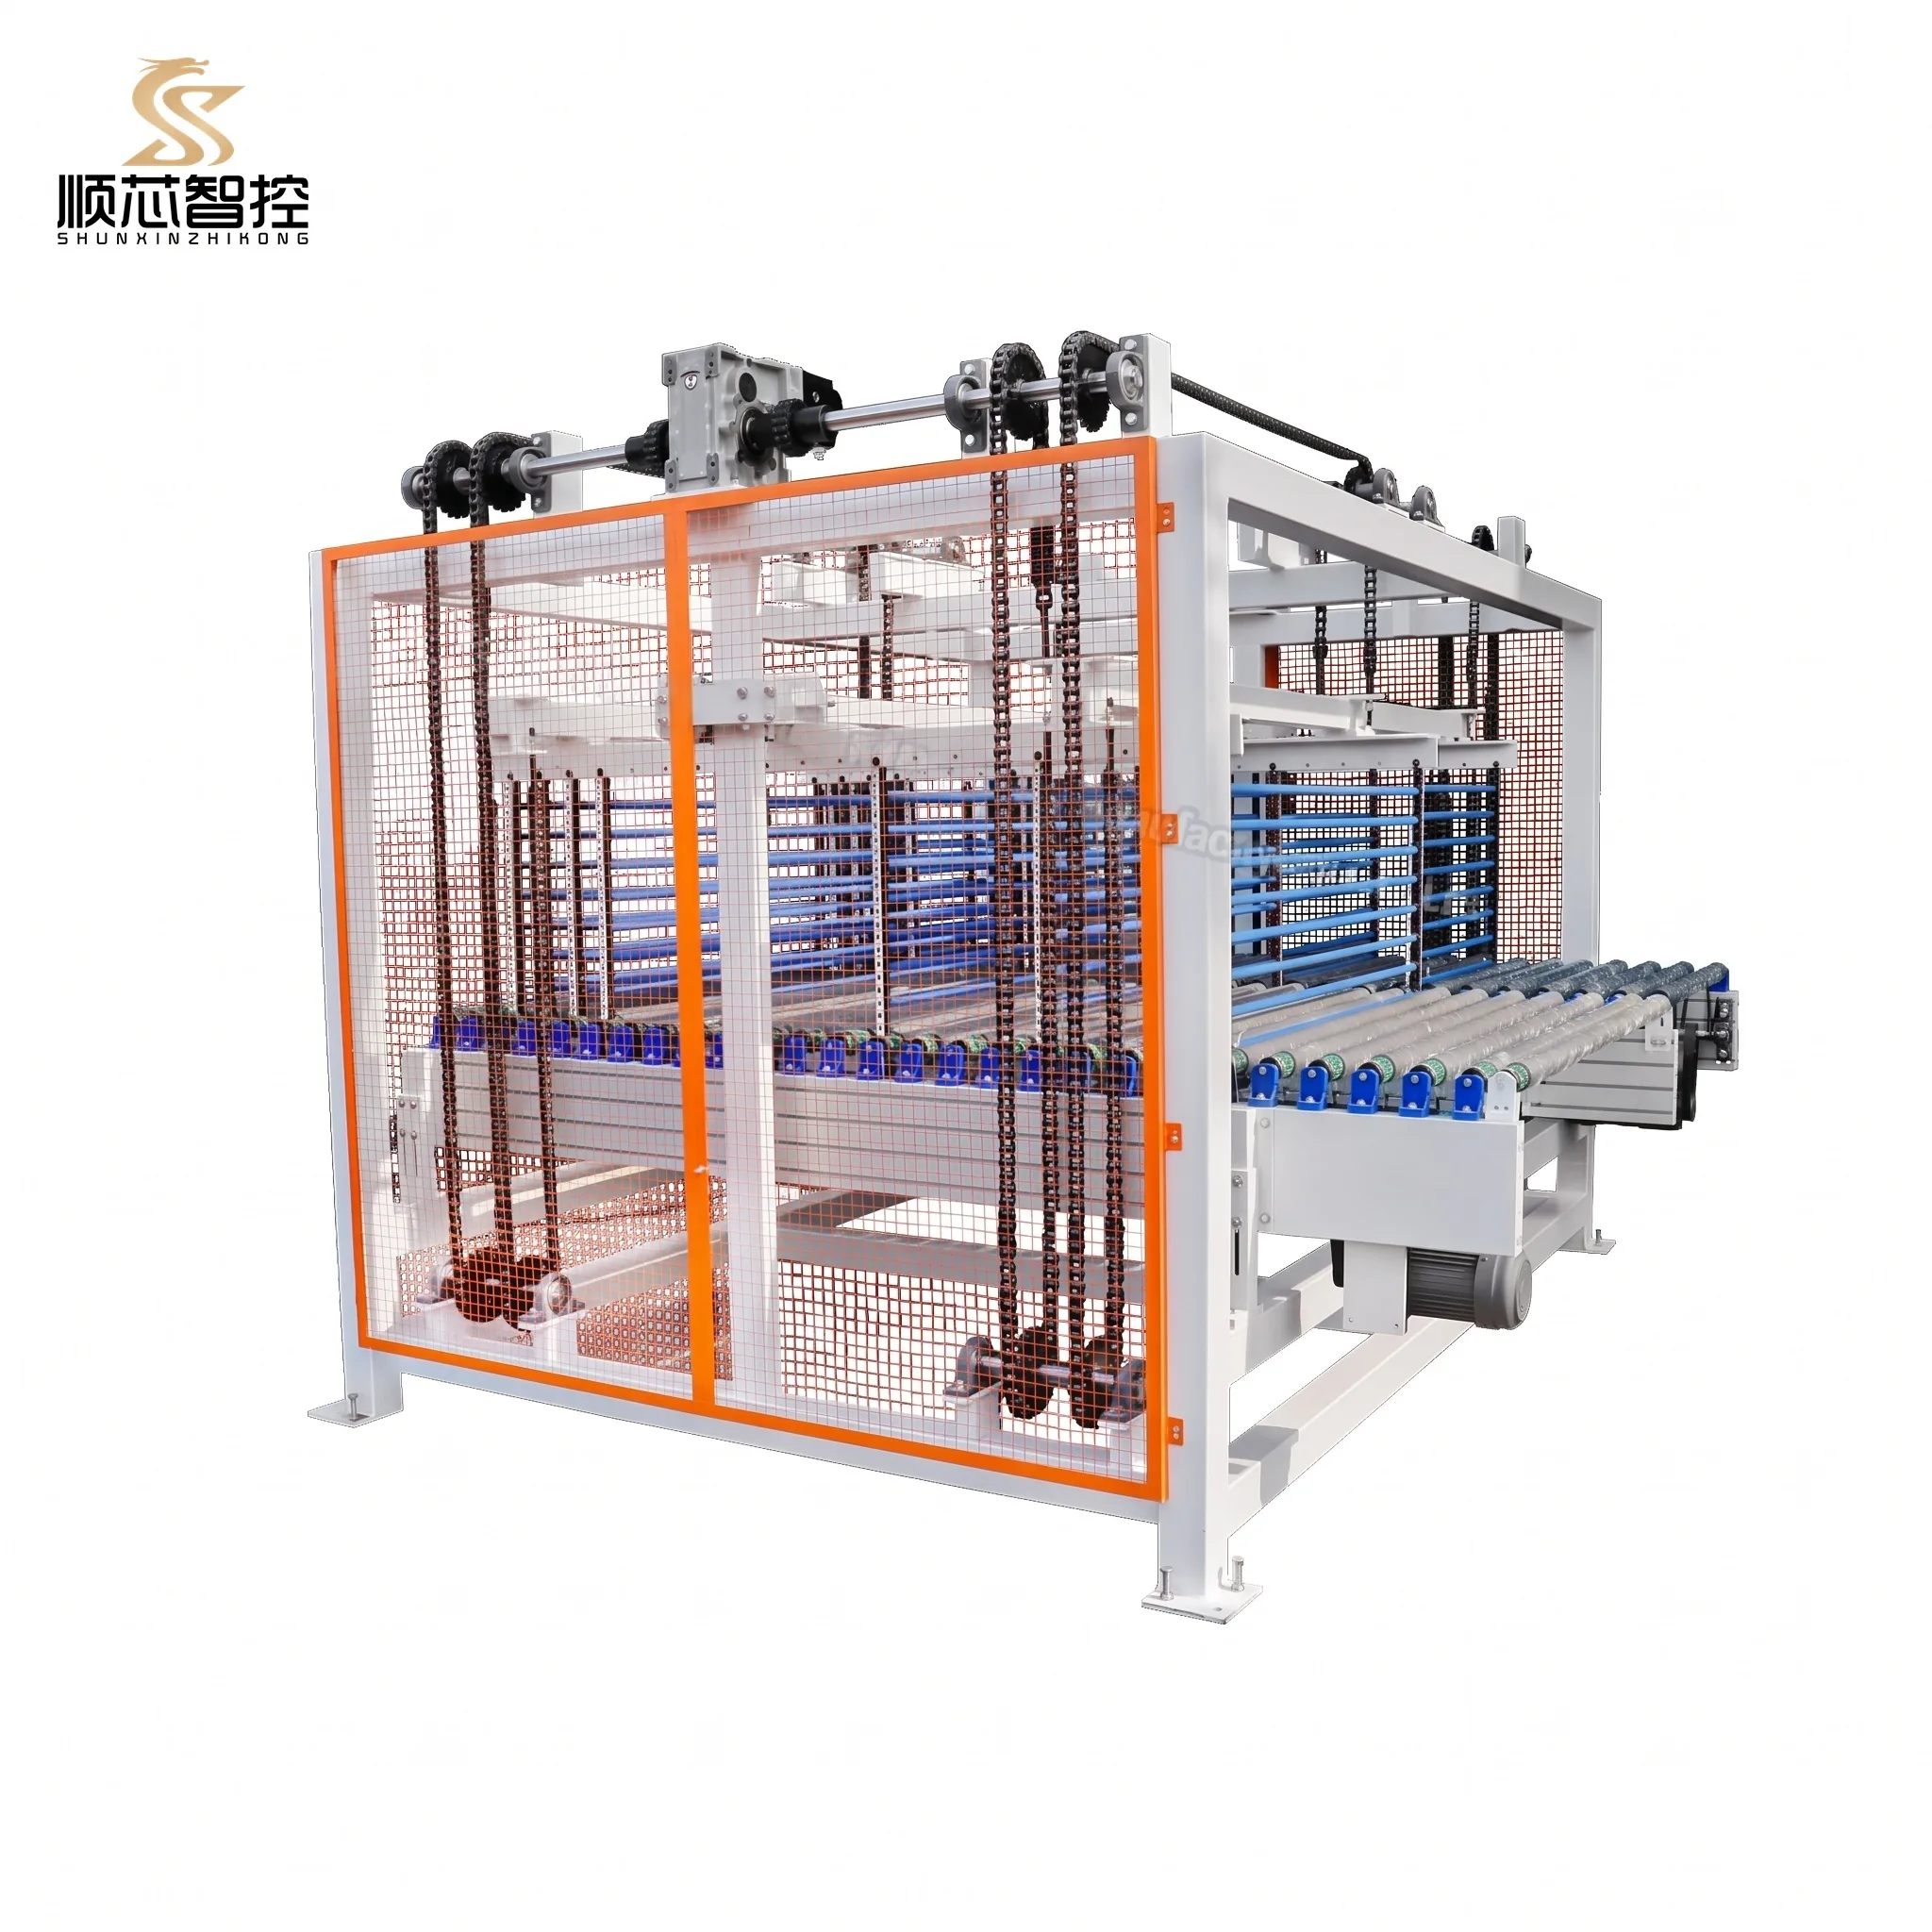
Serves as a temporary vertical buffer between nesting discharge and the edge bander. Organizes cabinet boxes by barcode job order, preventing floor congestion.
Global Industrial & GEO Export Standards for Turnkey Woodworking Lines
International manufacturing plants in North America, Europe, Southeast Asia, and the Middle East require equipment designed for regional standards:
GEO STANDARDS International Factory Integration Matrix
- Power Grid: 480V / 208V, 60Hz 3-Phase dual-wound motors
- Standards: UL 508A compliant control panels, NFPA 79 safety circuits
- Board Sizes: Standard 4×8 ft (1220×2440 mm) & 5×10 ft (1525×3050 mm) handling
<div class="p-3 rounded-xl bg-slate-900 border border-slate-800/80">
  <div class="font-bold text-white mb-1 flex items-center gap-2">
    <span class="w-2 h-2 rounded-full bg-emerald-400"></span>
    European Union (Germany, Poland, Italy, UK)
  </div>
  <ul class="space-y-1 text-slate-400 list-disc list-inside">
    <li>Power Grid: 400V, 50Hz with IE3 premium efficiency motors</li>
    <li>Safety Directive: CE Machinery Directive 2006/42/EC, light curtain guarding</li>
    <li>MES/ERP: Barcode/QR optical readers compatible with imos, TopSolid, and 2020 Design</li>
  </ul>
</div>

<div class="p-3 rounded-xl bg-slate-900 border border-slate-800/80">
  <div class="font-bold text-white mb-1 flex items-center gap-2">
    <span class="w-2 h-2 rounded-full bg-amber-400"></span>
    Southeast Asia (Vietnam, Malaysia, Indonesia Furniture Hubs)
  </div>
  <ul class="space-y-1 text-slate-400 list-disc list-inside">
    <li>Power Grid: 380V, 50Hz standard Asian industrial grid</li>
    <li>Climate Resistance: Anti-humidity tropicalized polyurethane conveyor belts</li>
    <li>Throughput Target: Engineered for 10-12 hour continuous mass production shifts</li>
  </ul>
</div>

<div class="p-3 rounded-xl bg-slate-900 border border-slate-800/80">
  <div class="font-bold text-white mb-1 flex items-center gap-2">
    <span class="w-2 h-2 rounded-full bg-purple-400"></span>
    Ocean Sea Freight & Packaging Standards
  </div>
  <ul class="space-y-1 text-slate-400 list-disc list-inside">
    <li>Crating: ISPM-15 certified heat-treated solid timber packaging</li>
    <li>Sealing: Multi-layer vacuum foil wrapping with industrial desiccant packets</li>
    <li>Container Loading: Modular knocked-down subassemblies fit standard 40HQ ocean containers</li>
  </ul>
</div>
4-Step Action Plan to Balance Your Cutting and Edge Banding Cells
Implement Smart Nesting Batching in CAM Software
Configure your nesting software (such as AlphaCAM, Cabinet Vision, or PolyBoard) to group parts by edge banding tape thickness and color, avoiding frequent tape changeovers on the bander.
Install Automatic Infeed Scissor Lift on CNC
Eliminate manual sheet lifting. An automatic hydraulic lift table keeps the raw board stack aligned with the CNC bed, reducing sheet loading time from 90 seconds to under 15 seconds.
Deploy an Accumulating Buffer Conveyor or Vertical Rack
Provide an intermediate holding station between the CNC discharge and the edge bander. This absorbs burst outputs from the router and feeds panels smoothly at the operator's pace.
Retrofit Edge Bander with a U-Loop Return Conveyor
Enable one operator to handle all four passes independently. Returning boards right to the feeder's hands eliminates outfeed catching and doubles daily throughput.
Production Line Balance Calculation Table
| Machine Station | Standalone Manual Flow | Automated Synchronized Flow | Improvement Metric |
|---|---|---|---|
| CNC Sheet Loading Time | 75 - 120 seconds (2 workers) | 18 seconds (Automated Scissor Lift) | -80% Loading Time |
| WIP Transfer Method | Manual wooden carts / Pallets | Motorized powered roller bed | Zero Floor Clutter |
| Edge Bander Manning | 3 Workers (1 infeed, 2 outfeed) | 1 Operator (U-Loop Return Line) | Save 2 Workers |
| Daily Panel Output (8h) | 650 – 800 finished panels | 1,400 – 1,800 finished panels | +115% Production Volume |
| Edge Defect / Scuff Rate | 2.1% (Manual trolley scuffs) | 0.2% (Air-cushion gliding) | -90% Scrap Losses |
Summary & Plant Engineering Support
Balancing high-speed nesting CNC cutting with linear edge banding is the cornerstone of profitable panel furniture manufacturing. By introducing automated infeed tables, buffering conveyors, and single-operator return loops, workshops eliminate bottlenecks while reducing labor overhead.
Contact our intralogistics engineering team today with your workshop layout and daily sheet processing targets to receive custom 2D/3D plant flow simulations and turnkey equipment quotations.
All automated loop return procedures and electrical sensor alignments must adhere to standard workshop lockout-tagout (LOTO) protocols and host machinery manufacturer guidelines. Shunxin equipment includes universal dry-contact interlocks to ensure immediate emergency stop response across synchronized production lines.
Need a Custom Layout Drawing & Quotation for Your Workshop?
Send us your workshop dimensions or CAD floor plan. Our mechanical engineers will deliver a synchronized layout proposal and payback calculation within 24 hours.